
- Home
- Products
- Solutions
- Projects
- Demo
- Support
- Training
- Contact Us
Get a Free Quote
+91 9910835218
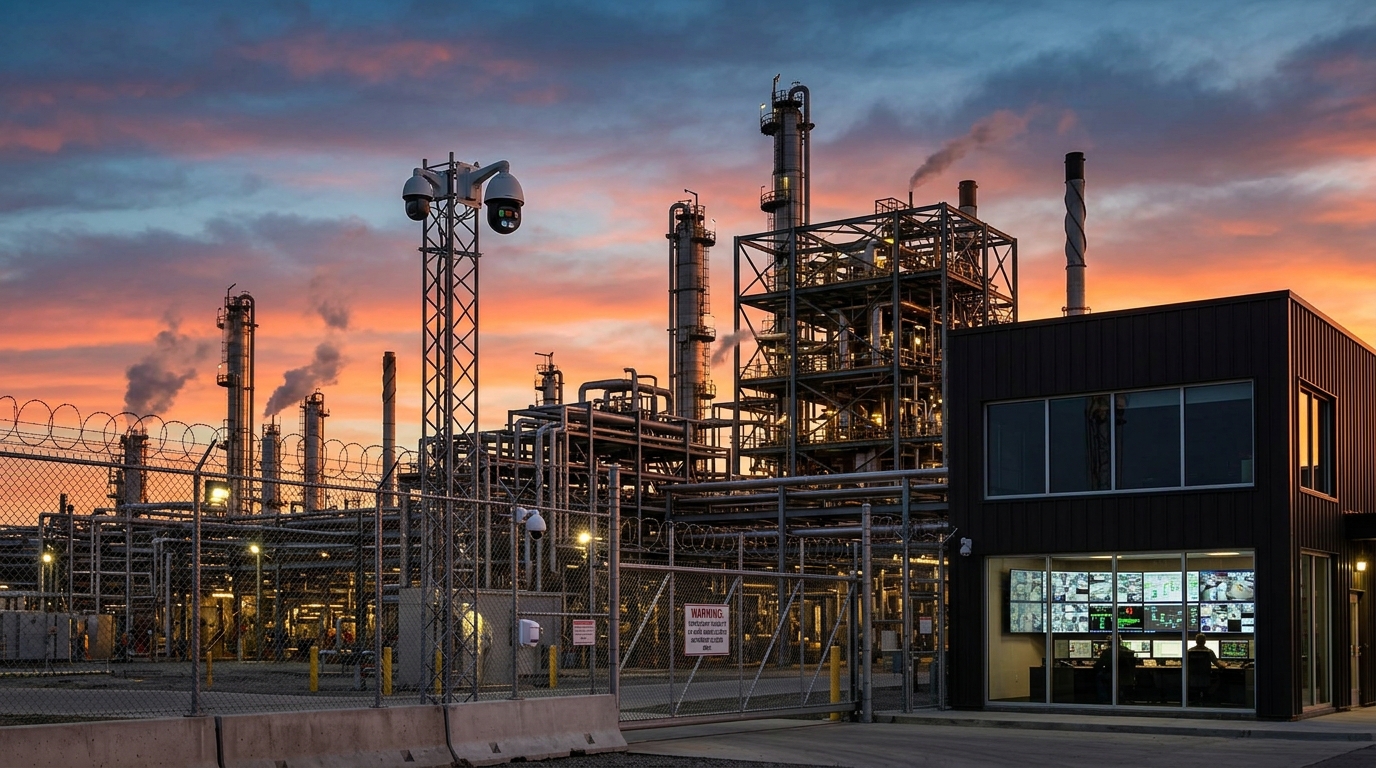
Turnkey electronic security for pharmaceutical, chemical, and precision engineering complexes.
Hazardous materials handling, flammable vapors, stringent cleanroom access limits, and meeting ISO/OSHA statutory security audit standards.
We supply ATEX-certified flameproof cameras, cleanroom airtight access interlocks, perimeter fiber-optic fence sensors, and unified SCADA-integrated alarm systems.
Discuss your facility layout, camera count, and data retention requirements with our security architecture specialists.
Request Solution ConsultationIndustrial plant safety monitoring, worker PPE detection, assembly line tracking, and heavy machinery security...
Explore Solution →Logistics hub surveillance, loading bay barcode sync, aisle high-bay CCTV, and automated perimeter patrol....
Explore Solution →Solar-powered wireless surveillance, temporary site fencing alarms, and building material theft prevention....
Explore Solution →Connect directly with our security architects and commercial sales team for custom proposals.
Thank you! Your quotation request has been received. Our technical sales team will review your requirements and reach out promptly.
Please verify your details once to watch this video. You'll receive 120 minutes of uninterrupted access to all videos in this section.